Compare automatic and semi-automatic mineral water plant systems based on production requirements, manpower, workflow, scalability and operational needs to determine...
With Pune experiencing rapid suburban development and industrial migration across manufacturing belts like Pimpri-Chinchwad and Ranjangaon, the commercial demand for packaged drinking water has scaled exponentially. Establishing a competitive venture requires robust machinery capable of continuous daily output while strictly matching Bureau of Indian Standards (BIS) parameters.
Our manufacturing plant in Vatva, Ahmedabad specializes in fabricating complete turnkey mineral water project lines shipped directly to Pune. By cutting out local distributors and engineering every component in-house, we provide complete transparency, sturdy stainless steel construction, and optimum capital efficiency for new plant owners.
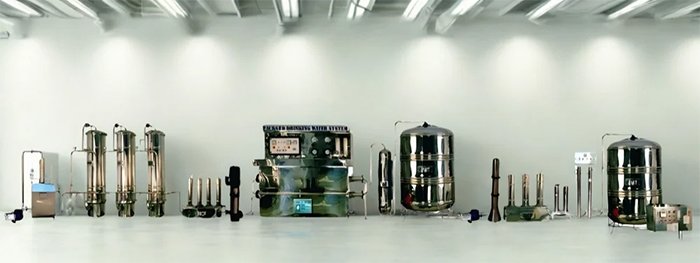
A fully integrated production line engineered for optimal purity, safety, and operational efficiency.
Multi-grade filters (MGF) and activated carbon filters (ACF) designed to remove suspended solids, chlorine, turbidity, and unpleasant odors from raw borewell or municipal supply.
High-rejection commercial RO plants engineered to drastically reduce Total Dissolved Solids (TDS), heavy metals, and microscopic impurities while maintaining high water recovery rates.
Precise mineral adjustment systems to balance essential minerals (magnesium and calcium) followed by UV sterilization and ozone generators to ensure absolute microbial safety.
Rotary and linear monoblock machines constructed from food-grade stainless steel (SS304/SS316) to handle PET bottle washing, precise gravity filling, and secure screw capping.
Bypass dealer markups and invest directly in robust machinery built in Vatva, Ahmedabad.
Equipment engineered to assist you easily clear government and quality inspection norms.
Experienced technical crew handles complete plumbing, electrical alignment, and trial runs.
Corrosion-resistant stainless steel liquid contact parts ensuring absolute product purity.
We build customized plants ranging from compact setups producing 1,000 liters per hour (LPH) up to heavy industrial systems delivering 5,000+ LPH based on your market demand in Pune.
Yes. Our engineering team provides detailed floor layouts, piping schematics, and electrical load requirements tailored to your factory space in Pune.
You can instantly connect with our engineering consultants via call or WhatsApp at **+91 70161 31099** to review your raw water lab analysis.
Explore our expert technical guides to help you plan, license, and scale your packaged drinking water business.

Compare automatic and semi-automatic mineral water plant systems based on production requirements, manpower, workflow, scalability and operational needs to determine...

Learn how water moves through a mineral water production facility, including pretreatment, filtration, reverse osmosis, disinfection, treated water storage and...
Discover the essential factors beyond machine capacity that determine the long-term profitability of a mineral water plant. Learn how to...
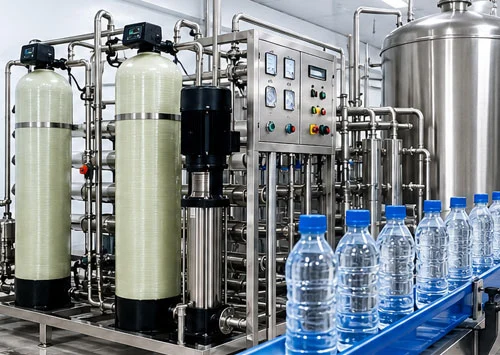
A complete technical equipment breakdown of industrial mineral water plant machinery, covering food-grade SS 304/316 purification skids, automatic 3-in-1 bottling...
A commercial guide to starting a mineral water plant business, featuring capital investment breakdowns, operational costs, profit margins per bottle,...
The ultimate master guide to starting a packaged drinking water manufacturing plant, covering the complete purification process, BIS/FSSAI licensing requirements,...
Consult with our project engineers in Vatva, Ahmedabad to evaluate your budget, factory footprint, and capacity requirements.
Users Today : 7
Users This Month : 1336
Total Users : 1337