Compare automatic and semi-automatic mineral water plant systems based on production requirements, manpower, workflow, scalability and operational needs to determine...
Build a high-volume water bottling and packaging business across the Mumbai Metropolitan Region, Thane, and the Thane-Belapur industrial belt with precision systems built in Vatva, Ahmedabad.
As the primary commercial and financial powerhouse of western India, the Mumbai Metropolitan Region (MMR)—including Thane, Kalyan, Bhiwandi, and Navi Mumbai—sustains an immense, non-stop commercial demand for packaged drinking water. Establishing a profitable and sanitary bottling plant within this fast-paced market requires resilient machinery that guarantees zero downtime and strict compliance with national health codes.
Our manufacturing facility located in Vatva, Ahmedabad specializes in building complete, turnkey mineral water purification lines and automated bottling monoblocks shipped directly to your factory floor in Thane or Mumbai. By designing and fabricating every component under one roof, we eliminate middleman overheads and ensure absolute quality control.
Heavy-duty FRP filtration vessels configured to remove suspended silt, organic impurities, residual tastes, and unpleasant odors prior to fine membrane filtration.
Advanced reverse osmosis systems built to balance raw Total Dissolved Solids (TDS) efficiently while conserving water and power resources.
Precision mineral addition loops to restore essential beneficial minerals, backed by UV sterilization chambers and ozone contact tanks for absolute pathogen safety.
Compact, high-speed rotary monoblock structures fabricated from premium SS304/SS316 steel to manage container washing, precise volumetric filling, and sealing.
Receive heavy machinery straight from our Vatva, Ahmedabad production floor without distributor margins.
Plant architecture designed to match mandatory Bureau of Indian Standards (BIS) water guidelines.
Our expert technicians travel to Mumbai and Thane for complete mechanical setup and trial runs.
All liquid-handling pathways utilize non-reactive food-grade stainless steel assemblies.
We configure scalable processing capacities ranging from 1,000 LPH (Liters Per Hour) compact units up to 5,000+ LPH industrial bottling factories.
We arrange secure, insured logistics directly from our Vatva workshop to your designated warehouse or factory site across the Mumbai-Thane region.
You can instantly consult with our senior technical advisors via phone or WhatsApp at **+91 70161 31099** to review your lab parameters.
Explore our expert technical guides to help you plan, license, and scale your packaged drinking water business.

Compare automatic and semi-automatic mineral water plant systems based on production requirements, manpower, workflow, scalability and operational needs to determine...

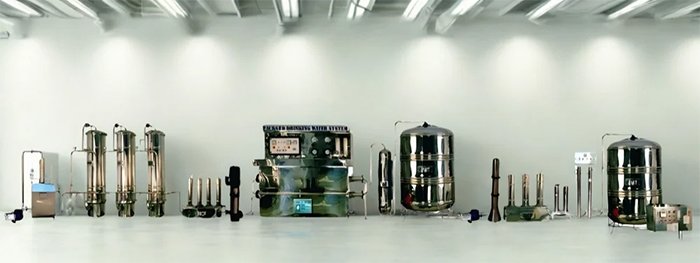
Learn how water moves through a mineral water production facility, including pretreatment, filtration, reverse osmosis, disinfection, treated water storage and...
Discover the essential factors beyond machine capacity that determine the long-term profitability of a mineral water plant. Learn how to...
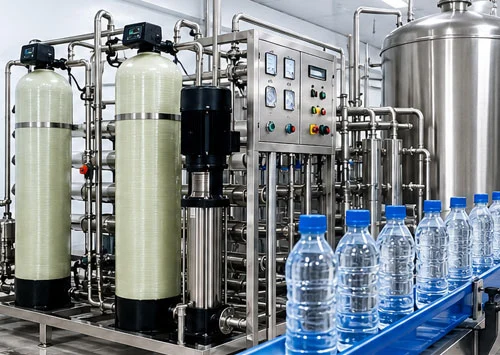
A complete technical equipment breakdown of industrial mineral water plant machinery, covering food-grade SS 304/316 purification skids, automatic 3-in-1 bottling...
A commercial guide to starting a mineral water plant business, featuring capital investment breakdowns, operational costs, profit margins per bottle,...
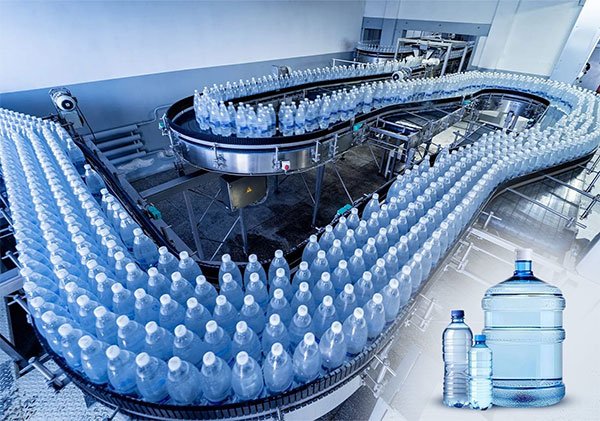
The ultimate master guide to starting a packaged drinking water manufacturing plant, covering the complete purification process, BIS/FSSAI licensing requirements,...
Speak directly with our plant design engineers in Vatva, Ahmedabad to evaluate your budget and floor space blueprint.
Users Today : 3
Users This Month : 1640
Total Users : 1641